News
Nov. 16, 2026
Choosing a conveyor for an Automotive Painting System means balancing production rate, paint quality, plant layout, worker safety, maintenance, and long-term cost. A system that moves vehicles efficiently in assembly may not perform well in a paint shop, where temperature, humidity, overspray, cleaning chemicals, and contamination control affect equipment selection. This guide gives purchasing groups a practical step-by-step method for defining requirements, comparing options, and checking supplier proposals. Jingzhongjing Group shares this guidance to help teams plan a conveyor solution that fits their coating process and production goals.

List every vehicle body, component, or carrier that will travel through the system. Record the product length, width, height, weight, center of gravity, and approved lifting or suspension points. Include the largest and heaviest product, not only the average one. Note whether product dimensions or models are expected to change during the conveyor's service life. These details establish the required clearance, hanger or skid design, allowable load, and ability to handle different product families.
Start with the target number of units per shift and the available production hours. Account for planned breaks, changeovers, cleaning, and expected downtime. Convert the target into a takt time, which is the time available to complete one unit at the required rate. Then confirm whether the conveyor must run continuously, index products at stations, or support a mixture of both. Ask production and operations teams to verify that the target reflects realistic line availability, not only the theoretical maximum.
Calculate the maximum combined load of the product, carrier, fixtures, and any attached equipment. Determine minimum product spacing at curves, inclines, station stops, and process transitions. Check whether the system must carry one product per carrier or several components on a shared carrier. Confirm how loads are distributed and whether dynamic forces during starts, stops, or elevation changes affect the design. The conveyor supplier should use the worst-case load and spacing values when sizing components.
Gather these items before requesting proposals. Missing information can lead to assumptions, change orders, and equipment that does not fit the process.
Do not select a conveyor type by name alone. Compare how each option handles the product, process conditions, layout, and maintenance access.
Ask what happens when a booth, oven, inspection station, or downstream process stops. The proposed system should state where products can accumulate, how much buffer is available, and which equipment controls the release of carriers. Confirm that accumulation does not cause product contact, excessive dwell time, paint quality issues, or unsafe congestion. Request a clear description of normal operation, controlled stops, emergency stops, and restart behavior.
Review the hanger, skid, fixture, or carrier interface with production and paint-quality teams. It must support the product securely while exposing the required surfaces to cleaning, pretreatment, painting, and curing. Confirm that the carrier can tolerate process temperatures and cleaning chemicals, and that its geometry does not create unacceptable shadowing, contamination traps, or paint buildup. Define how carriers will be identified, inspected, cleaned, and replaced.
Create a process sequence showing loading, pretreatment, drying, painting, flash-off, curing, cooling, inspection, repair, and unloading as applicable. Record the required dwell time, speed, temperature exposure, and operating conditions at each stage. The conveyor supplier should confirm that the selected speed and carrier spacing can maintain the process requirements throughout the route. Include rework and bypass paths where the production plan requires them.
Ovens and paint areas place demands on conveyor components that do not apply in ordinary material handling. Check the rated operating temperature of chains, bearings, lubricants, carriers, sensors, cables, and drive components. Ask how expansion, lubrication, and component wear are managed across temperature changes. In wet or chemically aggressive areas, confirm corrosion protection and material compatibility. In paint zones, discuss contamination control, overspray buildup, cleaning access, and measures that reduce the risk of particles reaching finished surfaces.
Agree on the product orientation and movement needed to achieve consistent coating coverage. Review vibration, swinging, rotation, acceleration, and stopping behavior because these can affect application quality and product handling. Establish acceptable limits with the paint-process and quality teams. Ask the supplier to explain how the design avoids contact marks, collision risks, excessive carrier movement, and sources of oil, dust, or debris near the coating process.
Compare the calculated production rate with the time each product must spend in each process zone. For a continuous conveyor, confirm that the operating speed and zone length provide the required dwell time. For indexed or accumulation sections, confirm that the control sequence preserves process timing and product spacing. Have process engineering and the conveyor supplier review the calculations together, especially where a speed change affects an oven, booth, or transfer point.
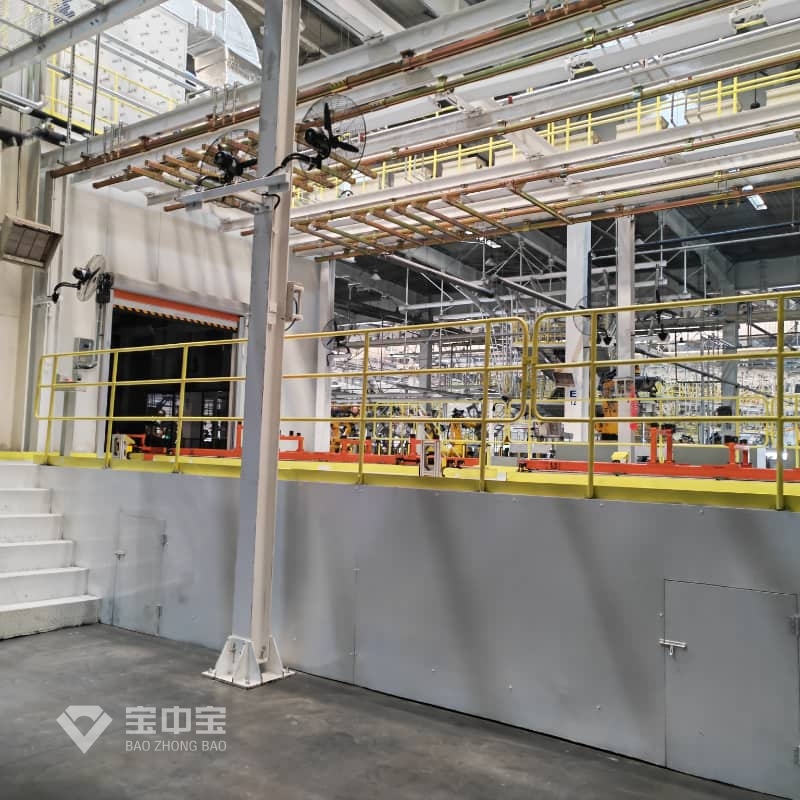
Use the current plant layout to check the conveyor route, elevations, curves, transfers, maintenance platforms, and structural supports. Verify clearances around buildings, columns, ducts, fire protection equipment, lighting, and other production assets. Check the product's full swept envelope through curves and elevation changes, including the carrier and any movement of the load. Make sure operators and maintenance staff can reach inspection points without creating unsafe access conditions.
Identify bottlenecks and determine how much buffer is needed upstream and downstream of critical equipment. Examine every transfer between conveyor types and every point where products stop, merge, split, or change elevation. Ask how a failed carrier, blocked route, or equipment fault can be isolated and recovered. A good layout should make routine inspection possible and should not require an entire line shutdown for every minor intervention.
Document required operating modes, such as automatic production, manual movement, maintenance, and recovery. Specify how the conveyor will communicate with booth, oven, fire protection, and plant control systems. Agree on alarm priorities, fault messages, carrier tracking, production counts, and data access. Confirm how a line stop is managed and how the system prevents an unexpected restart. Include the required backup, access control, and change-management procedures for control software.
Ask the supplier to identify pinch points, moving loads, elevated equipment, maintenance access hazards, and areas where operators may interact with the conveyor. Review guarding, emergency stops, safe access, lockout procedures, and safe recovery of a stopped carrier with the site safety team. Confirm that the design aligns with applicable local codes and the plant's standards. Review fire protection, ventilation, drainage, and any environmental controls that affect the route or equipment.
Request a preventive maintenance schedule covering inspection intervals, lubrication, chain or track checks, carrier inspection, drive components, sensors, and control backups. Confirm which tasks can be completed by plant technicians and which require specialist support. Ask for recommended critical spares, delivery lead times, service response terms, training, and manuals. Maintenance teams should review whether components are accessible and replaceable without disrupting adjacent equipment or exposing staff to process hazards.
Give each bidder the same product data, process sequence, layout, production targets, and site requirements. Ask each supplier to identify assumptions, exclusions, scope boundaries, and items that the plant must provide. A proposal should describe the conveyor concept, rated capacity, carrier design, speed range, accumulation strategy, controls, safety provisions, installation scope, and commissioning plan. Require suppliers to list any information they still need instead of allowing unclear assumptions to become hidden risks.
Build a comparison that includes equipment, engineering, installation, commissioning, utilities, maintenance labor, spare parts, cleaning, expected downtime, and future capacity changes. Review energy use and the cost of maintaining equipment under the actual paint-shop conditions. Ask each bidder to explain service coverage, warranty limits, spare-part availability, training, and performance guarantees. The lowest initial price may not be the lowest-cost option if it creates difficult maintenance or process interruptions.
Each group should review the proposal against its own requirements before final selection. Production should validate throughput and recovery plans. Process engineering should confirm dwell time and paint-process compatibility. Quality should check carrier design and contamination controls. Maintenance should review access and spare parts. Safety should assess guarding and work methods. Procurement and finance should compare scope, commercial terms, and lifecycle cost. Record open questions, assign an owner to each, and close them before approving the design.
Designing only for average weight, dimensions, or production rate can cause overloads, clearance conflicts, or throughput shortfalls. Use the worst-case product and realistic operating schedule, and have the relevant teams approve the assumptions.
A conveyor that meets a general material-handling specification may still fail to provide the required dwell time, temperature capability, cleanliness, or product presentation. Evaluate the whole route with paint-process and quality specialists.
Hard-to-reach components can increase downtime and create unsafe maintenance work. Overspray, lubricants, dust, and worn parts can threaten finish quality. Review access, cleaning, lubrication, and inspection methods during design, not after installation.
Vague terms such as high capacity or low maintenance are difficult to measure. Request defined design values, testing methods, acceptance criteria, and written responsibilities for installation, utilities, training, and commissioning. Confirm that performance commitments reflect the agreed product mix and operating conditions.
Selecting a conveyor for an Automotive Painting System is a cross-functional engineering and purchasing decision, not simply a choice of conveyor type. Use measured production data, validate the design against each paint-process stage, and compare suppliers on safety, maintainability, quality, and lifecycle cost. With requirements agreed before purchase, Jingzhongjing Group can help project teams move from a clear specification toward a conveyor solution suited to their Automotive Painting System.